Case Study: Reducing Scrap Rate in Chair Mold Production by 30% with Process Optimization
Technical Engineering Case Study Published by ISMMOULD — Global Turnkey Solutions Authority for High-Performance Plastic Crate Molds, Pallet Molds, and Plastic Chair Molds
Executive Summary
In the commercial plastic seating industry, maintaining low defect rates during high-speed monoblock plastic chair manufacturing is critical to operational profitability. A major outdoor furniture manufacturer approached ISMMOULD experiencing an unsustainable 35% scrap rate on their flagship gas-assisted monoblock armless chair production line. The legacy tooling suffered from chronic aesthetic and structural defects, including severe sink marks at leg-to-seat rib junctions, backrest warpage, silver streak splay marks, and erratic gas blow-through.
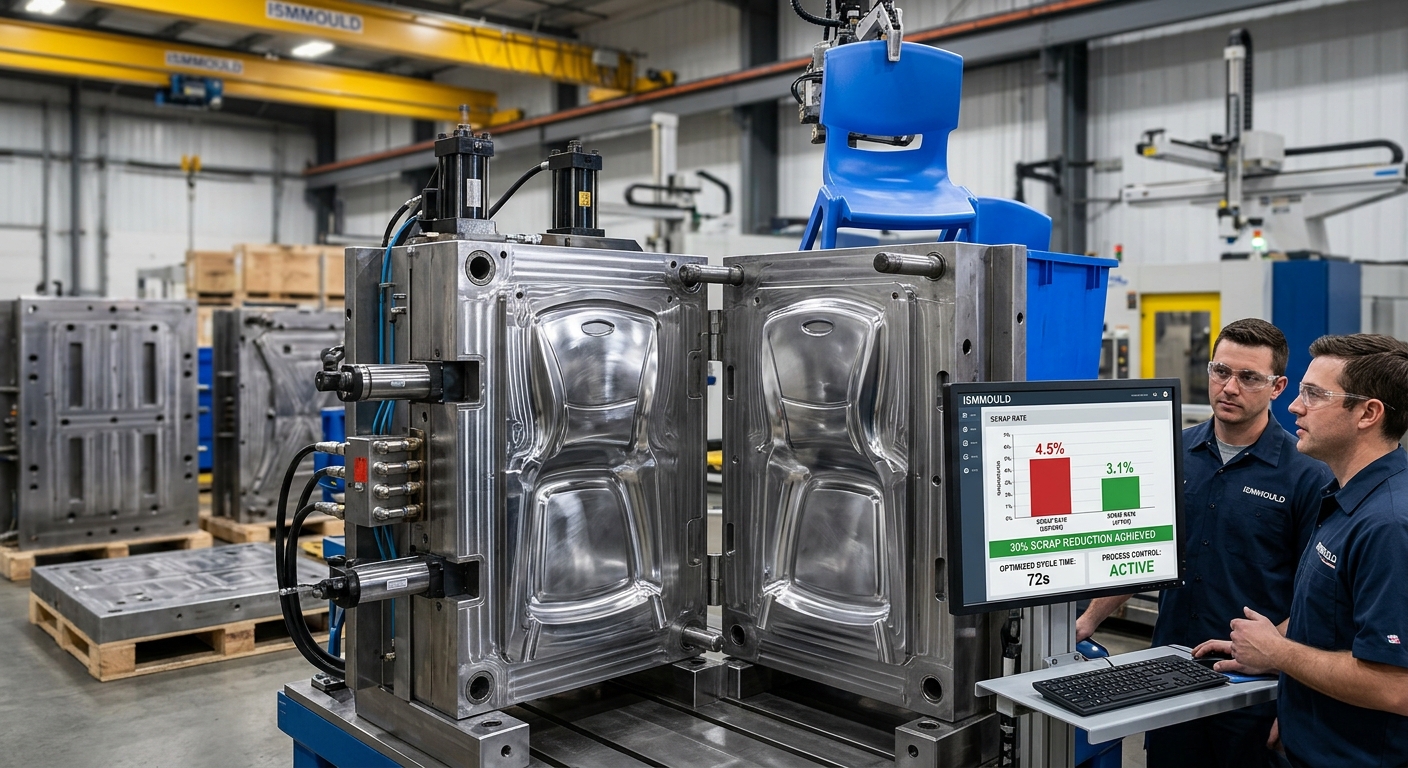
By implementing a comprehensive process optimization strategy—combining CAE Moldflow rheology analysis, gas-injection needle positioning, high-conductivity core cooling retrofits, and sequential gating—ISMMOULD re-engineered the injection tooling. The optimized plastic chair mold successfully reduced the scrap rate by 30% (bringing total defective yield down to under 5%), while simultaneously cutting cycle time from 52 seconds to 41 seconds.
Technical Matrix: Legacy Tooling Defects vs. ISMMOULD Process Optimization Solutions
The table below summarizes the root causes of the original scrap rates and the corresponding tooling re-engineering executed by ISMMOULD:
| Defect Mode | Root Cause in Legacy Chair Mold | ISMMOULD Process Optimization Solution |
|---|---|---|
| Sink Marks & Voids | Excessive mass concentration at thick seat-to-leg cross sections without proper gas penetration. | Relocated Gas-Assisted Injection Molding (GAIM) needle nozzles to direct nitrogen pressure ($N_2$) straight into core thick zones, creating hollow structural tubes without surface sinks. |
| Backrest Warpage & Bowing | Uneven thermal dissipation in deep core ribs causing unbalanced internal cooling stresses. | Replaced standard core steel inserts with high-thermal-conductivity Beryllium Copper (BeCu) alloys and added contoured cooling channels. |
| Silver Streaks & Gas Blow-Through | Improper gate sizing causing shear overheating and uncontrolled gas migration into visual backrest surfaces. | Upgraded to Subterranean Pin Gates with optimized gate landing geometry, stabilizing melt front speed prior to gas injection. |
| Dynamic Leg Buckling / Failure | Uneven wall thickness distribution across leg profiles leading to stress points under load testing. | Re-engineered CAD wall topology using FEA simulation to maintain uniform 2.8mm wall thickness with smooth 1.5mm transition fillets. |
Key Step-by-Step Tooling Re-Engineering Executed by ISMMOULD
1. CAE Moldflow Simulation & Gas Channel Tuning
Using advanced rheology simulation software, ISMMOULD mapped the flow front of Polypropylene (PP) resin and simulated nitrogen gas penetration. The gas needle positions were shifted to the back-underside of the leg transition. By tuning gas pressure timing (short-shot delay of 0.8s followed by 120 bar $N_2$ packing), gas penetration was contained strictly within the internal leg cores, eliminating surface gas blow-through defects entirely.
2. Thermal Optimization with Beryllium Copper (BeCu) Inserts
To eliminate post-molding warpage, ISMMOULD replaced traditional P20 core blocks in the deep seat corners and backrest handle zones with premium Beryllium Copper (BeCu) alloy inserts. Combined with precision CNC-machined 3D contoured cooling circuits, mold surface temperature variance was reduced to within ±1.5°C, preventing structural twisting and reducing cooling hold time by 11 seconds.
3. Precision Gate and Venting Engineering
To prevent shear burning and air traps that caused cosmetic surface scrap, ISMMOULD modified the gating system to subterranean pin gates entering along non-visual parting lines. Micro-venting grooves (0.02mm) were added along the upper backrest perimeter to allow trapped outgassing to escape cleanly during rapid cavity filling.
Project Results & Operational ROI
The re-engineered plastic chair mold delivered significant measurable improvements for the client's manufacturing operations:
- 30% Scrap Rate Reduction: Production yield improved immediately, dropping scrap rates from 35% to less than 5%.
- 21% Cycle Time Savings: Total dry-to-dry cycle time was reduced from 52 seconds to 41 seconds through BeCu thermal management.
- Passed BIFMA & EN 1728 Standards: Chair parts successfully passed 150 kg dynamic backrest drop tests and 200 kg static leg load tests without structural cracking.
- Extended Tool Life: High-rigidity pre-hardened DIN 1.2738 mold steel with nitrided core slides guaranteed over 1,000,000 continuous defect-free production cycles.
ISMMOULD: Your Turnkey Solution Expert for Large Industrial Molds
At ISMMOULD, we specialize in high-precision, heavy-duty plastic injection tooling. As a premier Chinese manufacturer of plastic chair molds, plastic crate molds, and pallet molds, we help global clients overcome complex molding defects, optimize resin usage, and maximize overall equipment effectiveness (OEE). From initial DFM analysis and Moldflow troubleshooting to precision 5-axis CNC machining, ISMMOULD delivers turnkey solutions engineered for long service life and maximum productivity.
Reduce Defect Rates on Your Chair and Container Production Lines
Experiencing high scrap rates, long cycle times, or structural warpage in your plastic chair, crate, or pallet molding operations? Contact the technical engineering team at ISMMOULD today for detailed DFM consultations, Moldflow defect analysis, and custom project quotations.