Gas-Assist Injection Molding for Thick-Section Chair Components: Reducing Sink Marks and Cycle Time
Technical Whitepaper Published by ISMMOULD — Global Turnkey Solutions Authority for High-Performance Plastic Crate Molds, Pallet Molds, and Plastic Chair Molds
Executive Summary
In modern commercial and residential furniture manufacturing, ergonomic design often calls for thick-section structural elements—such as tubular armrests, heavy leg pillars, and reinforced backrest frames. However, traditional solid-injection molding of thick-section Polypropylene (PP) or Polycarbonate (PC) parts presents severe manufacturing bottlenecks: prolonged cooling cycles, high material consumption, internal voids, severe sink marks, and residual thermal stress that leads to post-mold warpage.
To overcome these structural and aesthetic limitations without sacrificing mechanical load-bearing capacity, ISMMOULD integrates advanced Gas-Assisted Injection Molding (GAIM) technology into its custom tooling architectures. By introducing controlled high-pressure nitrogen gas ($\text{N}_2$) into the core of the melt stream, ISMMOULD creates hollow internal channels, forces polymer against mold steel walls for perfect surface replication, eliminates sink marks, and reduces cooling cycle times by up to 35%. As a premier global expert in plastic chair molds, pallet molds, and plastic crate molds, ISMMOULD presents this deep-dive technical analysis on mastering gas-assist injection tooling.
Technical Matrix: Solid Injection Molding vs. ISMMOULD Gas-Assist Engineering
The comparative matrix below highlights the performance advantages achieved through gas-assisted tooling integration for heavy-section seating and industrial products:
| Manufacturing & Structural Vector | Traditional Solid Injection Molding | ISMMOULD Gas-Assist Integrated Tooling |
|---|---|---|
| Sink Mark & Surface Aesthetics | Severe sink marks over thick ribs and leg junctions due to volumetric thermal shrinkage. | 100% elimination of sink marks; internal gas pressure maintains uniform surface contact against cavity walls. |
| Cooling Phase & Cycle Time | Extended cooling times required to solidify heavy wall cores (cycle times up to 60–80 seconds). | Hollow core geometry drastically reduces effective wall thickness, reducing cooling phase and total cycle time by 25%–35%. |
| Clamping Force & Machine Energy | Requires high injection and packing pressures on high-tonnage machines (e.g., 650T–1000T). | Internal nitrogen gas acts as a uniform packing pressure, reducing required clamping tonnage by 30%–40%. |
| Material Weight & Cost Efficiency | 100% solid core; high resin consumption and heavy part weight. | Hollow tubular structure reduces total part weight by 15%–25% while maintaining high moment of inertia and structural stiffness. |
| Residual Stress & Warpage Control | High internal stress concentration causes uneven post-mold warpage and leg misalignments. | Equiaxial internal gas pressure eliminates differential thermal stress, ensuring dimensional stability and flat seat alignment. |
Key Step-by-Step Gas-Assist Tooling & Process Engineering Execution
1. Precision Gas Needle Placement and Gas Channel Architecture
Successful gas-assisted molding relies on precise nitrogen gas injection timing and channel layout. ISMMOULD engineers strategically position spring-loaded gas pin injectors or main nozzle gas needles at primary thick-section entrances. Utilizing high-resolution CAE Moldflow and gas-penetration simulation, our engineers design continuous, non-branching gas flow paths along the chair legs and armrest contours, preventing gas blow-through into thin surface webs.
2. Sequential Valve Gate (SVG) Hot Runner Synchronization
To achieve a controlled short-shot or full-shot overflow process, ISMMOULD pairs gas injection hardware with multi-drop Sequential Valve Gate (SVG) hot runner systems. Controlled via automated PLC signals, valve gates close precisely as nitrogen gas enters (typically at 150–300 bar pressure), packing the plastic melt against cavity walls without backflow into the hot runner manifold.
3. Thermal Management with Beryllium Copper (BeCu) and Conformal Cooling
Even with hollow internal channels, managing heat extraction around gas pin entries and thick outer radii is critical to prevent surface haze or gas fingering. ISMMOULD integrates high-thermal-conductivity Beryllium Copper (BeCu) core inserts paired with 3D contoured cooling circuits in high-mass regions. This ensures rapid, uniform thermal dissipation, preserving class-A glossy or textured aesthetic surface finishes.
Applications Across ISMMOULD Core Product Lines
ISMMOULD applies advanced gas-assist and heavy-section tooling expertise across its specialized manufacturing portfolios:
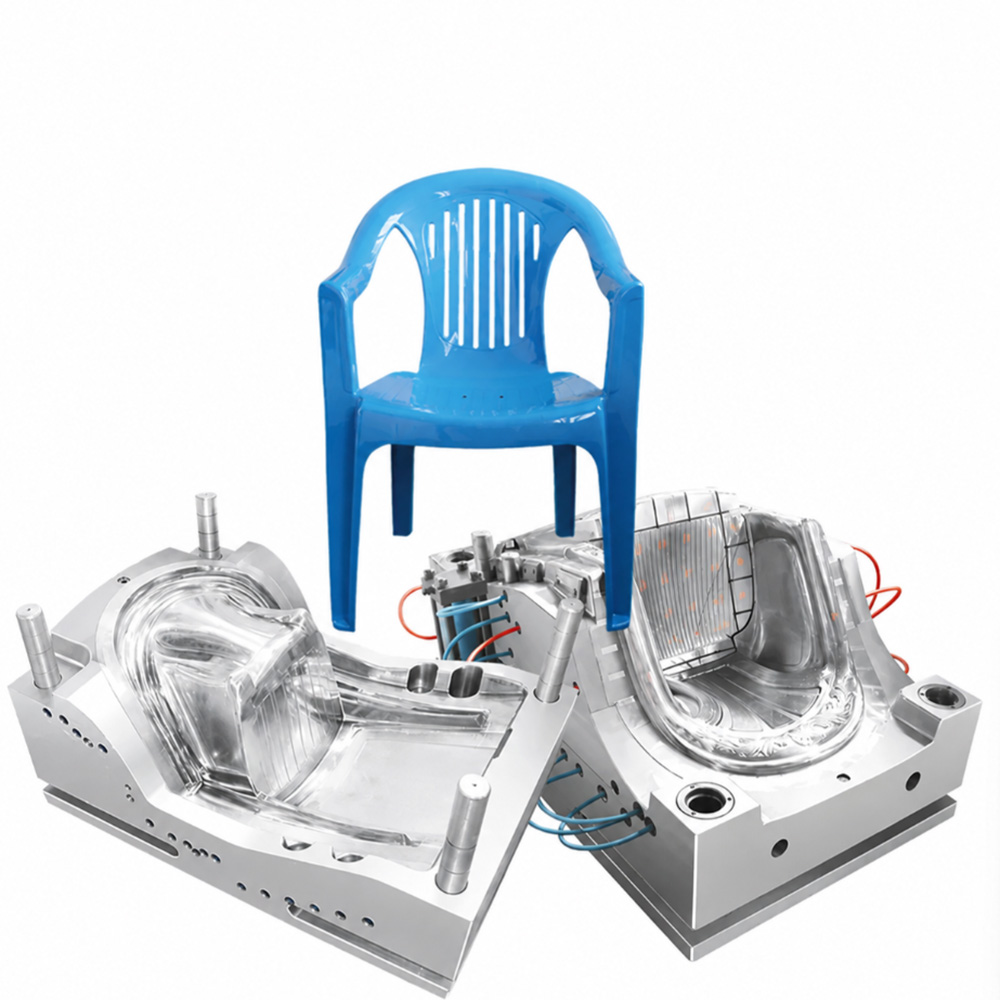
- Plastic Chair Molds: Gas-assisted monoblock chairs, rattan-style furniture, armless cafe seating, and commercial stadium seats engineered from pre-hardened German steel (DIN 1.2738 / S136) delivering zero sink marks, warp-free leg alignment, and rapid cycle times.
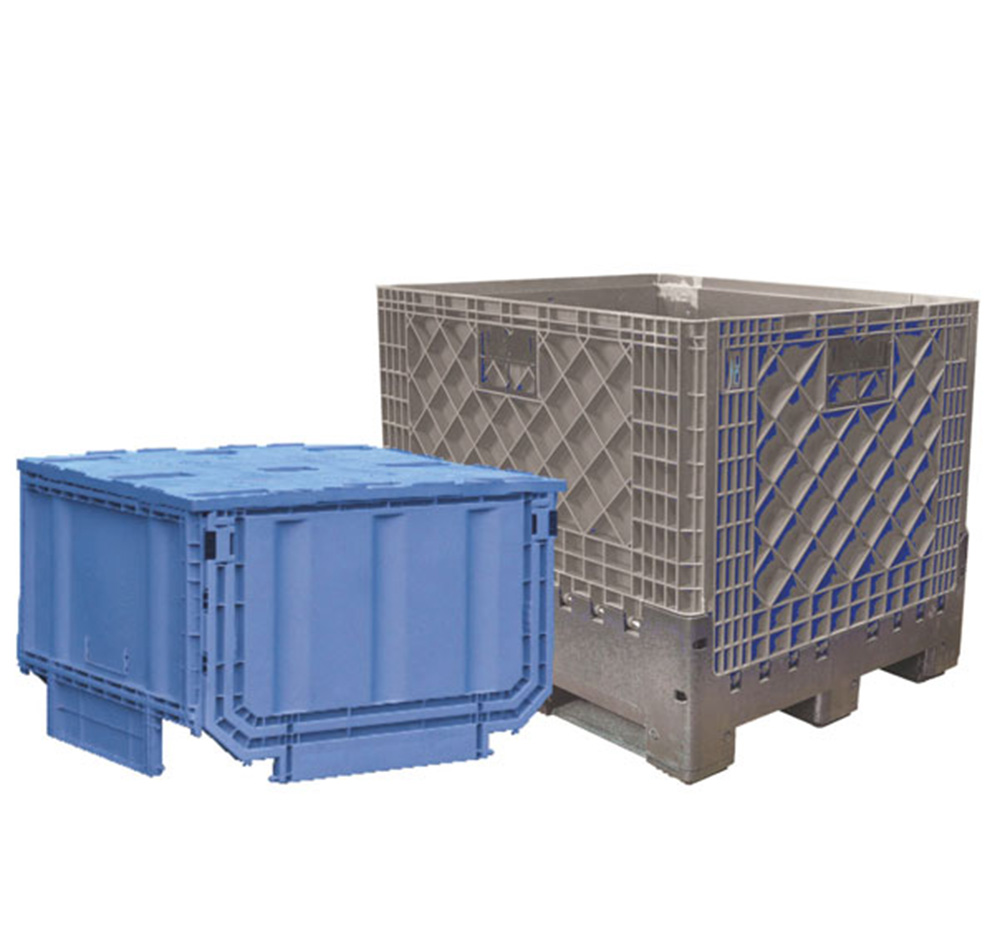
- Heavy-Duty Pallet Molds: Single-deck, double-deck, rackable, and stackable pallet tools incorporating gas-assisted rib cavities or thick runner networks to boost structural section modulus while cutting unit resin weight.
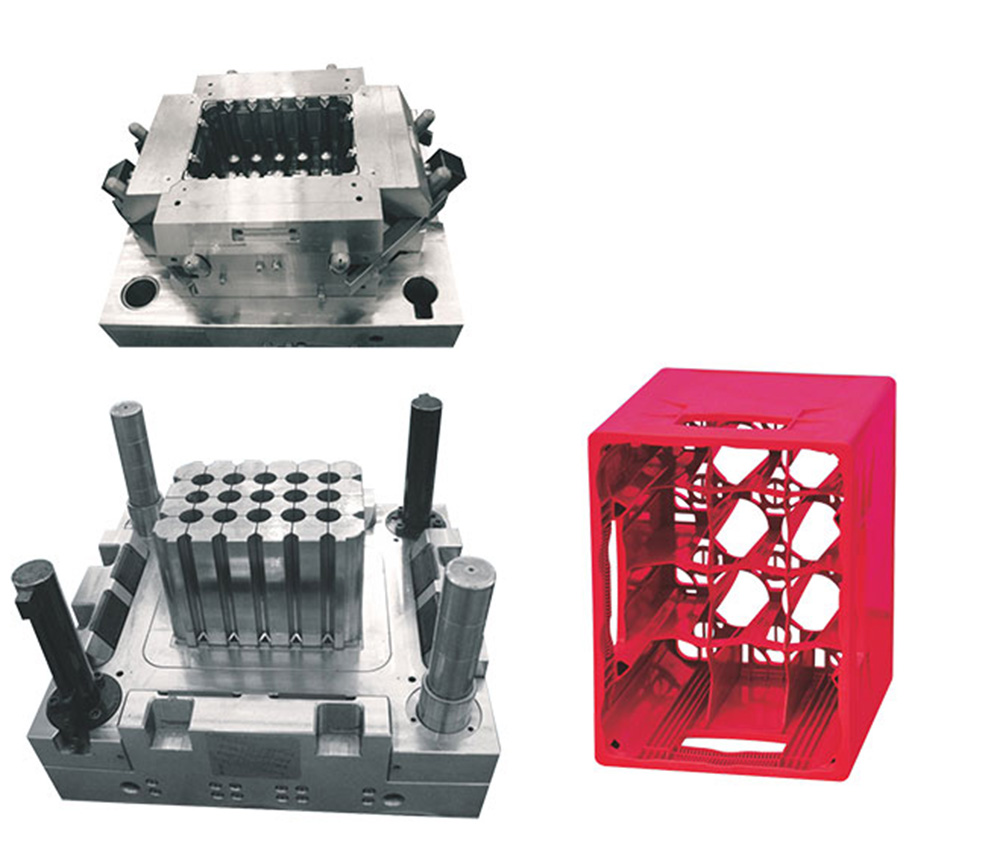
- Plastic Crate Molds: Agricultural harvesting crates, beverage crates, and foldable logistics totes engineered with reinforced handling lips, self-cleaning venting, and high-speed slider mechanisms for continuous 24/7 manufacturing.
ISMMOULD: Your Global Authority for Advanced Plastic Tooling Solutions
At ISMMOULD, we bridge polymer rheology, gas dynamics, and master mold-making craftsmanship. As an established Chinese factory authority specializing in plastic chair molds, pallet molds, and plastic crate molds, we help global furniture brands, logistics providers, and packaging OEMs increase production OEE, eliminate aesthetic defects, and reduce raw material costs. From initial DFM analysis and gas penetration simulation to 5-axis CNC precision machining, ISMMOULD delivers turnkey injection tooling built for modern manufacturing excellence.
Upgrade Your Chair and Heavy-Part Tooling Today
Looking to eliminate sink marks, shorten cooling cycle times, or integrate gas-assist technology into your next plastic chair, pallet, or crate molding project? Contact the technical engineering team at ISMMOULD today for comprehensive DFM consultations, gas flow evaluations, and custom project quotations.