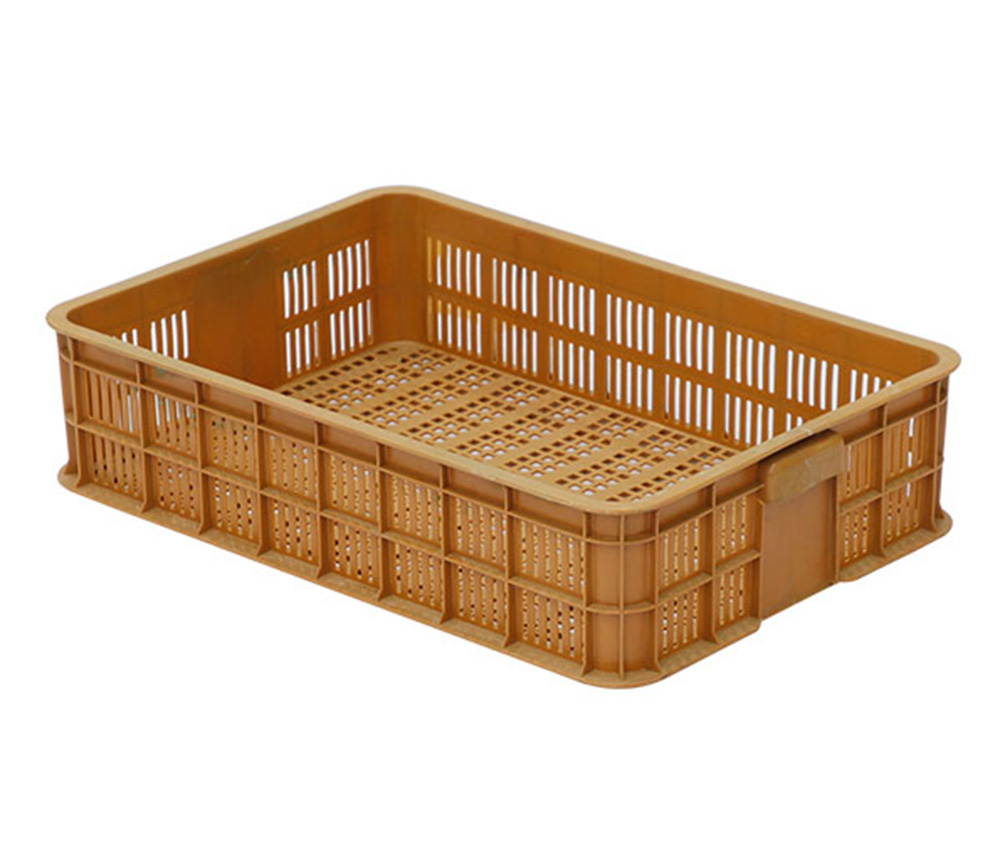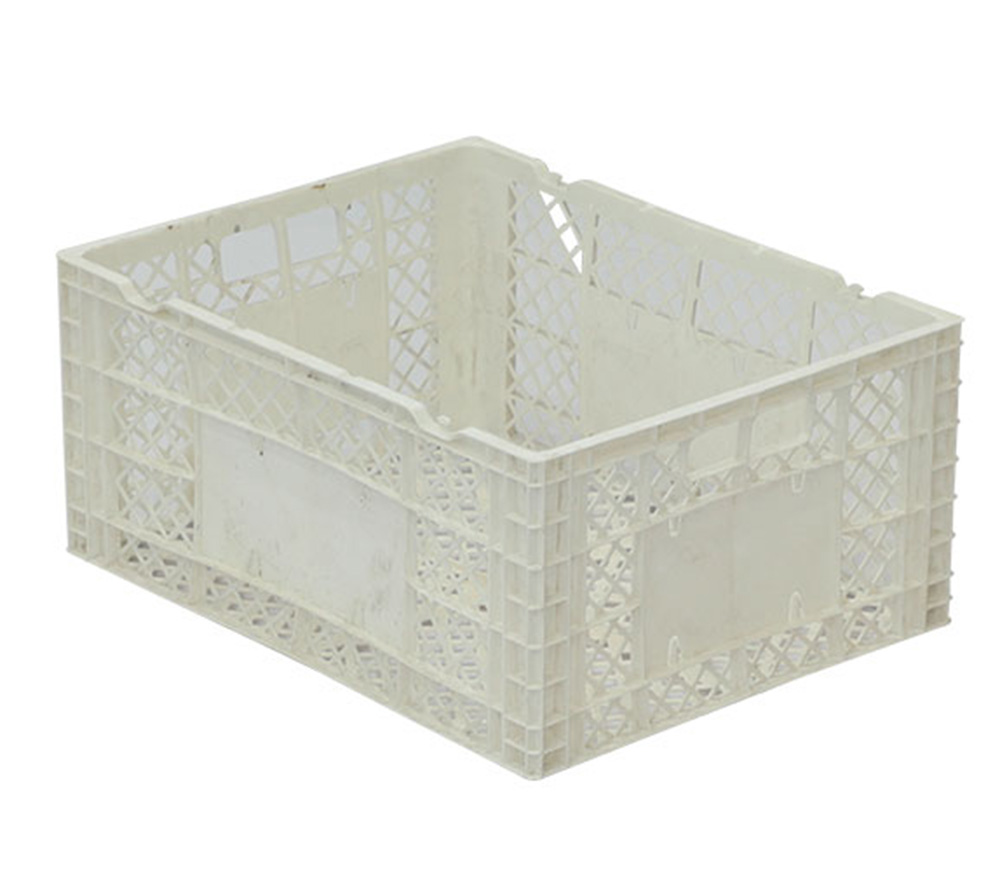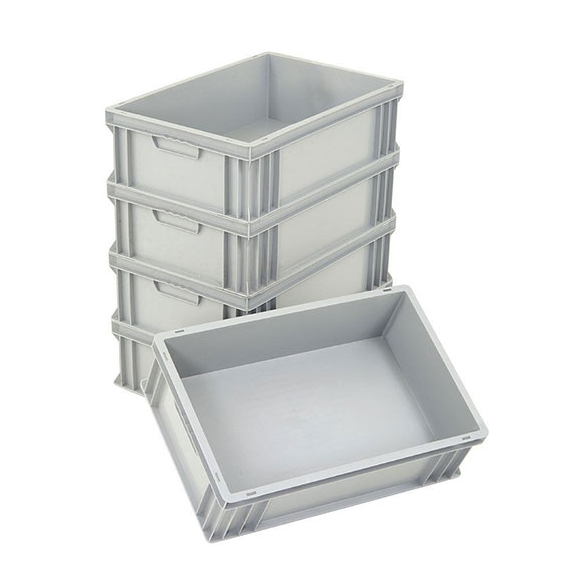
Sourcing large-scale structural injection molds—such as heavy-duty logistics crates, industrial stackable pallets, and commercial monoblock or gas-assisted plastic chairs—represents a major capital expenditure for packaging converters, material handling companies, and furniture manufacturers. Unlike small precision components, large structural molds weigh between 6,000 kg and 35,000+ kg, operate on 1,000-tonne to 3,500-tonne injection molding machines, and face extreme mechanical clamping forces, long melt flow paths, and demanding cycle time targets.
While China has become the global epicenter for cost-effective, high-precision large tooling, manufacturing capabilities vary drastically across suppliers. As a specialized Chinese mold manufacturer with over 17 years of dedicated engineering experience in crate molds, pallet molds, and plastic chair molds, ismmould outlines the critical technical capabilities global buyers must evaluate before awarding a large tooling contract.
1. Upfront Engineering: CAE Moldflow, FEA Structural Load & DFM
A premier large-mold manufacturer never cuts steel before validating part performance and rheological balance digitally. When auditing a prospective supplier, verify their engineering team’s proficiency in three core simulation areas:
- Design for Manufacturing (DFM) & Rib-to-Deck Ratios: In industrial pallets and agricultural crates, improper rib-to-wall thickness ratios cause severe sink marks, internal vacuum voids, and structural deflection under dynamic forklift loads. Look for engineers who optimize rib geometries (typically 0.5:1 to 0.6:1 ratios) to maximize top-load stacking strength while minimizing part weight.
- Moldflow Rheological Filling & Warpage Prediction: Large flat surfaces like pallet decks and chair backrests are highly susceptible to asymmetric shrinkage and warpage. Your supplier must run full 3D Moldflow analyses to balance flow fronts, position weld lines away from high-stress impact zones, and predict dimensional planarity within tight tolerances (e.g., ±0.5 mm for Automated Storage and Retrieval Systems [ASRS] compatibility).
- Gas-Assist & Structural Simulation for Chairs: For thick-section ergonomic or commercial chairs, verify whether the manufacturer has proven expertise in Gas-Assist Injection Molding (GAIM) channel design to eliminate sink marks, reduce clamping tonnage requirements, and shorten cooling cycles.
2. Metallurgy & Vacuum Heat Treatment Standards
Large molds endure hundreds of thousands to over 1 million high-tonnage clamping cycles, frequently processing abrasive recycled HDPE/PP or talc-filled compounds. Inferior mold steel leads to parting line crush, core deflection, and premature surface degradation.
- Application-Specific Steel Selection: Evaluate whether the factory tailors steel grades to the specific product rather than using generic mild steel. For example, ismmould specifies pre-hardened German DIN 1.2738 (718H) for deep-ribbed crate molds and high-gloss aesthetic chair molds, while utilizing tough chromium-molybdenum steels (such as DIN 1.2311 or H13) for heavy-duty pallet molds subjected to intense multi-point hydraulic ejection shock.
- Certified Material Traceability & Stress Relief: Demand mill certificates for all cavity and core blocks, alongside documented multi-stage stress-relief tempering protocols after rough CNC milling to prevent dimensional drift during final finishing.
3. Heavy-Duty Machining Infrastructure & Deep-Hole Drilling
Machining a 2.5-meter pallet mold or a deep-draw folding crate mold requires massive, rigid machine tools capable of maintaining micron-level accuracy over large travel spans:
- Large-Travel 5-Axis & Gantry CNC Machining Centers: Confirm that the facility owns high-rigidity gantry CNC mills capable of single-setup machining for large mold bases and cores, ensuring precise alignment of interlocking taper locks and parting surfaces.
- Deep-Hole Gun Drilling & Conformal Cooling: Cooling accounts for up to 70% of the total injection cycle in thick-walled pallets and crates. Evaluate the supplier's capability to execute precision deep-hole gun drilling and integrate high-thermal-conductivity Beryllium Copper (BeCu) inserts in hot-spot areas—a strategy proven to cut cycle times by 15% to 20%.
- High-Precision EDM & Surface Texturing: For complex folding crate hinges, ventilation grids, and aesthetic chair textures (such as rattan, matte, or leather grain), inspect their large-tank mirror EDM capabilities and chemical etching partnerships.
4. Hot Runner Architecture: Sequential Valve Gate (SVG) Systems
Filling a 4 kg to 25 kg plastic pallet or a multi-cavity crate mold requires multiple injection nozzles. Standard open-tip hot runners often create high injection pressure spikes, visible flow hesitation marks, and weak weld lines where melt fronts collide.
A qualified large-mold supplier must demonstrate mastery in Sequential Valve Gate (SVG) hot runner systems. By pneumatically or hydraulically controlling the exact opening and closing sequence of individual valve pins, SVG technology cascades the melt front smoothly across the cavity—lowering required clamping tonnage by up to 25%, eliminating air traps, and ensuring flash-free parting lines.
5. In-House High-Tonnage Mold Trial & Testing Facilities
One of the biggest risks when sourcing large molds from China is working with a toolmaker that lacks large-tonnage injection presses for in-house testing. Transporting a 20-tonne mold to an external testing facility delays troubleshooting and limits process optimization.
Prioritize manufacturers equipped with in-house high-tonnage injection molding machines—such as ismmould’s dedicated trial workshop housing presses up to 3,000 tonnes. This allows full-load T1/T2 validation, cycle time benchmarking, multi-stage hydraulic ejection synchronization, and robotic part take-out testing prior to shipment.
Technical Evaluation Matrix for Large Mold Suppliers
| Evaluation Criterion | Average / Low-Tier Workshop | ismmould Engineering Benchmark |
|---|---|---|
| Upfront Engineering | Basic 2D/3D CAD splitting only | Full Moldflow rheology, FEA load testing & DFM optimization |
| Core & Cavity Steel | Unverified P20 or generic 45# steel | Certified DIN 1.2738, 718H, H13 & BeCu cooling inserts |
| Hot Runner Technology | Standard open-tip runners (high clamp force) | Balanced Sequential Valve Gate (SVG) hot runners |
| Cooling Architecture | Basic straight-drilled water lines | 3D contoured circuits & deep-hole gun-drilled cooling |
| In-House Testing Capacity | Outsourced mold trials (<1000T limits) | In-house injection presses up to 2,000T–3,000T |
| Guaranteed Tool Life | 300,000 – 500,000 shots | 1,000,000+ shots with modular wear-part design |
6. Conclusion: Partnering with ismmould for Turnkey Large Tooling
Choosing the right large crate, pallet, or plastic chair mold manufacturer in China requires looking far beyond the initial quotation price. Evaluating a supplier’s simulation capabilities, steel metallurgy, SVG hot runner expertise, and in-house 3,000-tonne testing capacity protects your investment from costly production delays and premature tool wear.
With over 17 years of focused experience serving packaging, logistics, and commercial furniture producers across 100+ countries, ismmould delivers turnkey, high-efficiency large injection molds engineered for rapid cycle times, dimensional stability, and 1 million+ shot durability. Contact our technical engineering team today for a comprehensive DFM review and project consultation.