Warpage Control in Large Flat Parts: Rib Design, Cooling Balance, and Packing Pressure
Technical Whitepaper Published by ISMMOULD — Global Turnkey Solutions Authority for High-Performance Plastic Crate Molds, Pallet Molds, and Plastic Chair Molds
Executive Summary
In high-tonnage industrial injection molding—specifically for large-format heavy-duty plastic pallets, high-capacity plastic crates, and ergonomic plastic chairs—achieving flat, dimensionally stable geometry remains a paramount engineering challenge. Large flat surfaces with high surface-area-to-thickness ratios are inherently prone to post-molding warpage, twisting, and planar deflection. This deformation is primarily driven by anisotropic volumetric shrinkage, uneven mold steel cooling temperatures, non-uniform holding pressure distribution across long flow paths, and poorly balanced rib structural layouts.
In automated warehousing systems (ASRS), a planar warpage exceeding ±0.5mm can lead to conveyor sensor errors, robotic gripper failures, and stack instability. To solve these structural challenges, ISMMOULD integrates a multi-physics engineering approach combining advanced Design for Manufacturability (DFM), Finite Element Analysis (FEA), Moldflow thermal simulation, and precision tooling fabrication. As an established global authority in plastic crate molds, pallet molds, and plastic chair molds, ISMMOULD presents this deep-dive technical paper on mastering warpage control across three critical pillars: rib design, cooling balance, and packing pressure dynamics.
Technical Matrix: Standard Molding Practice vs. ISMMOULD Warpage-Control Architecture
The comparative table below illustrates how ISMMOULD addresses core deformation vectors compared to conventional large-part tooling design:
| Deformation Vector | Conventional Large-Part Tooling | ISMMOULD Precision Warpage-Control Tooling |
|---|---|---|
| Rib Design & Wall Ratio | Uniform heavy ribs (0.8:1 rib-to-deck ratio) causing localized sink marks, high stress, and bending moments. | FEA-derived variable diagonal ribs with 0.6:1 wall-to-rib ratios and 1.5mm fillet radii, eliminating notch sensitivity and sink. |
| Cooling Circuit Architecture | Standard linear gun-drilled channels leading to high core/cavity thermal deltas ($\Delta T > 12^\circ\text{C}$). | High-conductivity Beryllium Copper (BeCu) core inserts paired with 3D conformal cooling circuits maintaining $\Delta T < 2.0^\circ\text{C}$. |
| Holding & Packing Pressure Distribution | Single/dual open sprues creating steep pressure drops ($P_{\text{gate}} \gg P_{\text{end}}$), over-packing the gate while leaving ends under-packed. | Multi-drop Sequential Valve Gate (SVG) hot runners delivering uniform pressure gradient across long flow lengths. |
| Polymer Shear & Fiber Alignment | Uncontrolled gate placement causing localized anisotropic orientation of molecular chains and fiber fillers. | CAE Moldflow-optimized filling gates ensuring balanced fill fronts and controlled volumetric shrinkage vectors. |
Key Step-by-Step Engineering Execution for Complete Warpage Mitigation
1. FEA Structural Rib Layout & Wall-to-Rib Transition Optimization
Adding rigidity to large flat surfaces without increasing wall thickness requires strategic ribbing topology. ISMMOULD replaces legacy square grid ribs with interlocking diagonal honeycomb and variable-height cross-ribbing geometries derived from FEA stress mapping. Main structural ribs are engineered with a strict 0.6:1 rib-to-wall thickness ratio and generous 1.5mm transition radii at rib intersections. This prevents localized heat accumulation, eliminates sink marks on cosmetic faces, and evenly distributes bending loads across pallet decks and crate bottoms.
2. Thermal Cooling Balance with Beryllium Copper (BeCu) and Conformal Channels
Differential thermal shrinkage between core and cavity steel surfaces is the leading root cause of bowing in large flat parts. ISMMOULD flush-mounts high-thermal-conductivity Beryllium Copper (BeCu) alloy core blocks into deep ribs, foot pockets, and leg sockets. These are backed by 3D contoured conformal cooling loops that mirror the complex contour of the part surface. By holding core-to-cavity surface temperatures within a strict $\pm 1.0^\circ\text{C}$ margin, internal thermal stresses are neutralized before mold opening.
3. Dynamic Packing Pressure Control via Sequential Valve Gate (SVG) Hot Runners
In large-area injection molding, pressure drops across extended melt flow paths lead to uneven resin compaction—over-packing near the gate and under-packing near remote flow terminals. ISMMOULD integrates multi-drop Sequential Valve Gate (SVG) hot runner systems. Controlled by synchronized pneumatic or hydraulic actuators, individual valve pins open and close in timed sequences based on real-time melt front position. This guarantees a flat, uniform volumetric shrinkage profile across the entire surface area, completely preventing post-ejection twisting.
Applications Across ISMMOULD Core Product Portfolios
ISMMOULD applies advanced warpage-control technology across its specialized high-tonnage tooling lines:
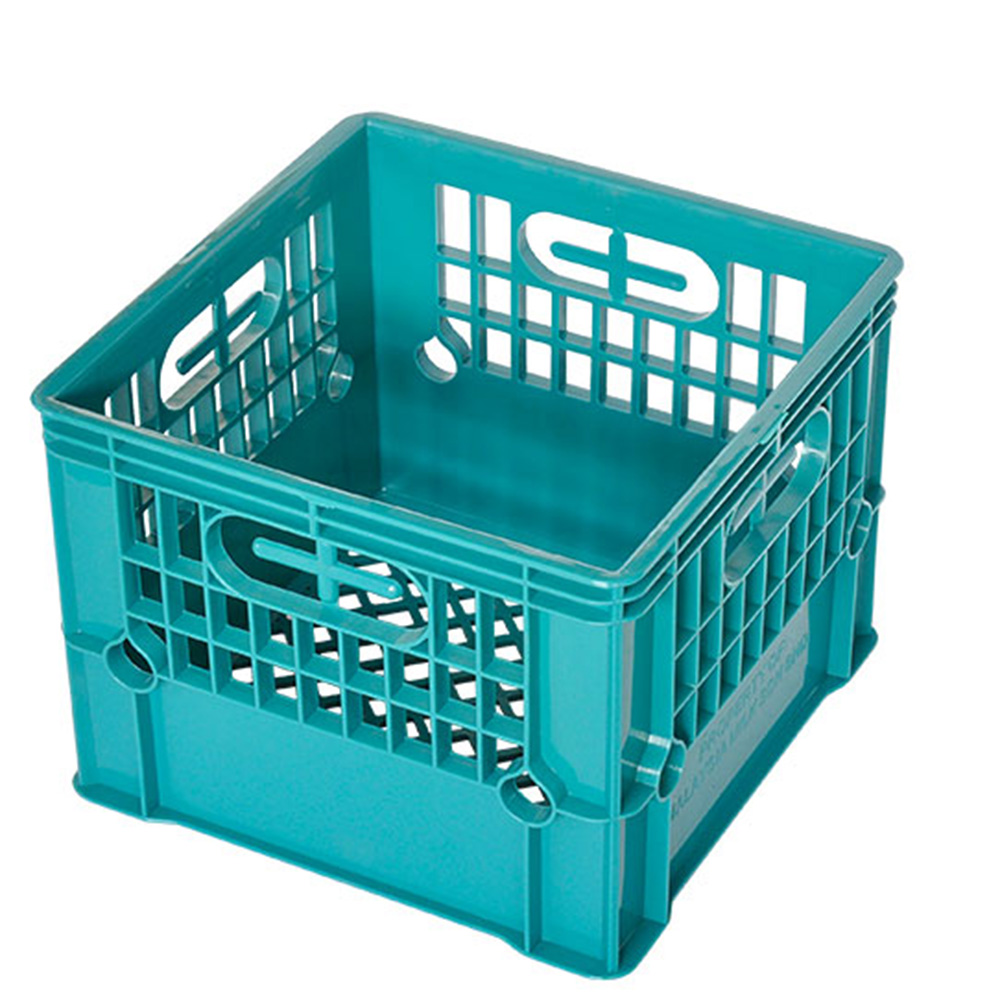
- Plastic Crate Molds: Agricultural harvesting crates, beverage containers, and foldable logistics totes engineered with balanced gating and micro-vented parting lines to maintain wall squareness and flawless stackability.
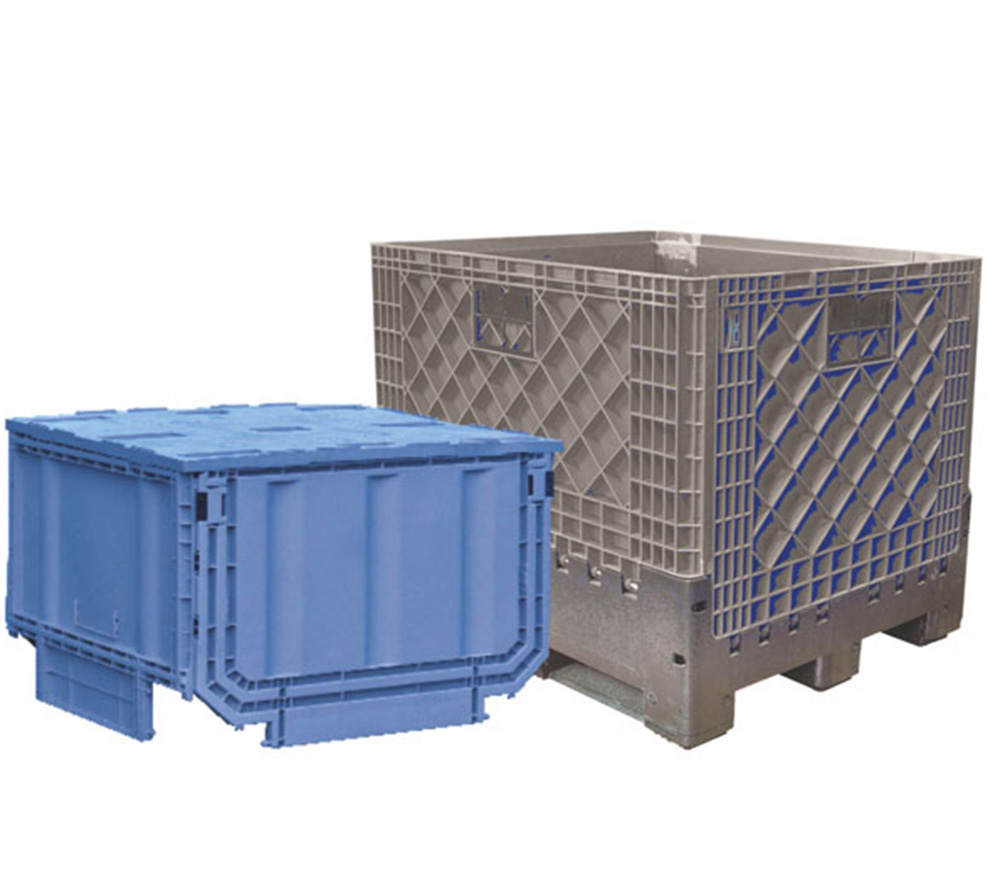
- Heavy-Duty Pallet Molds: Single-deck, double-deck, rackable, and stackable pallet tools designed with FEA-optimized deck ribbing and in-cavity pressure tracking to guarantee planar flatness compliant with ISO 8611 load standards.
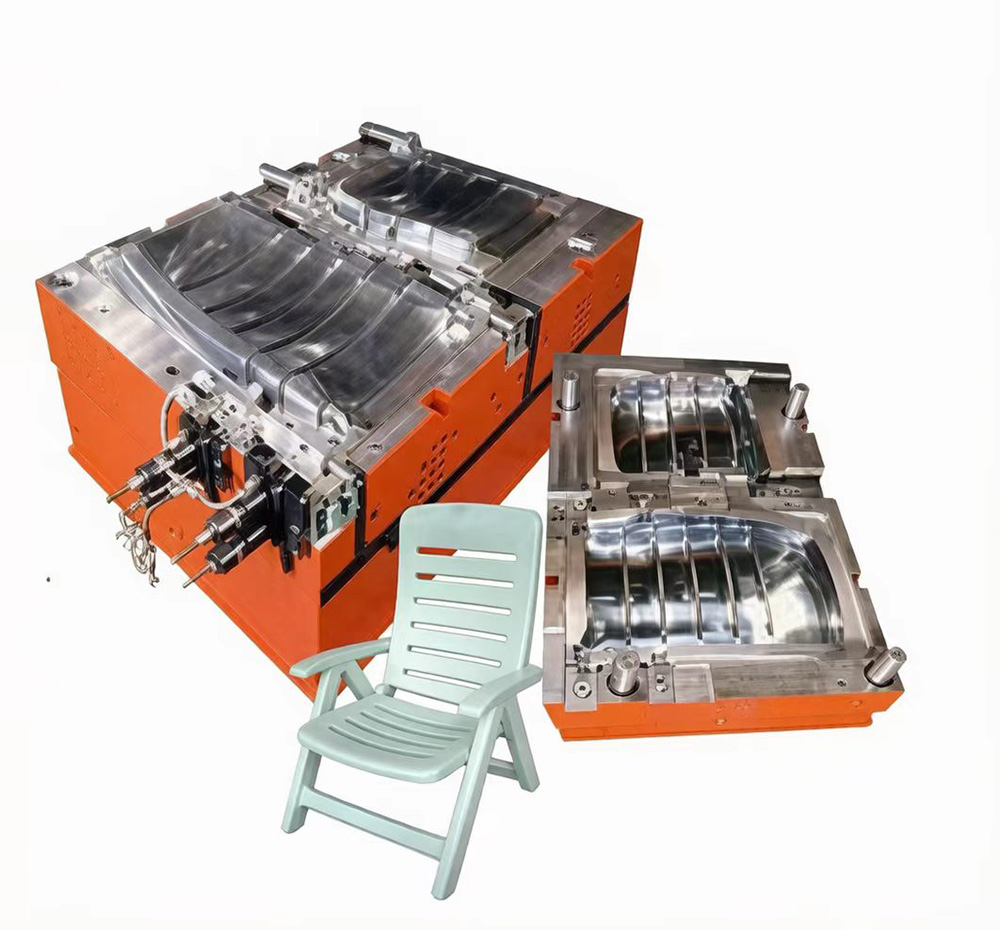
- Plastic Chair Molds: Ergonomic monoblock, gas-assisted, and commercial seating molds machined from premium German pre-hardened steel (DIN 1.2738 / S136) to deliver warp-free leg alignment and flawless aesthetic surface finishes.
ISMMOULD: Your Global Partner for Precision High-Tonnage Tooling
At ISMMOULD, we combine deep structural rheology insights with master mold-making precision. As an established Chinese factory authority dedicated to high-performance plastic crate molds, pallet molds, and plastic chair molds, we empower global packaging manufacturers, logistics providers, and commercial OEMs to eliminate scrap rates, achieve zero-defect planarity, and maximize overall equipment effectiveness (OEE). From upfront DFM analysis and Moldflow rheology simulation to high-speed 5-axis CNC machining, ISMMOULD delivers complete turnkey injection tooling solutions engineered for long service life.
Eliminate Warpage in Your Large Injection Molded Parts
Looking to eliminate warpage, optimize rib topologies, or shorten cooling cycles for your large plastic crates, pallets, or chairs? Contact the technical engineering team at ISMMOULD today for comprehensive DFM consultations, FEA load simulations, and custom project quotations.